The main 3D printer filament types are PLA, PETG, ABS, ASA, TPU, nylon, and polycarbonate, and each solves a different design problem. Choose by the part’s real job first: heat, impact, flexibility, outdoor exposure, surface finish, or dimensional accuracy. Then check whether your printer can supply the nozzle temperature, bed heat, enclosure, drying, and abrasion resistance the material requires.
Material behavior is easier to understand once extrusion, heat and layer formation are clear. This guide explains how 3D printers work before moving into the practical differences between filament types and settings.
- 3D printer filament types at a glance
- PLA: the sensible first material
- PETG: a tougher general-purpose option
- ABS and ASA: enclosed printing for functional parts
- TPU: flexible parts need a controlled filament path
- Nylon and polycarbonate: demanding materials for demanding parts
- Composite and specialty filaments
- Choose filament by the project, not the spool color
- Check printer compatibility before ordering a spool
- Drying and storage are part of material selection
- Treat temperature ranges as starting points
- Ventilation belongs in the print plan
- Common filament-selection mistakes
- Put the material choice into a real project
- 3D printer filament types FAQ
I treat filament as part of the design brief, not a color decision made after the model is finished. A thin snap-fit, a sunlit bracket, and a display maquette may share the same geometry, but they should not automatically share the same plastic.
3D printer filament types at a glance
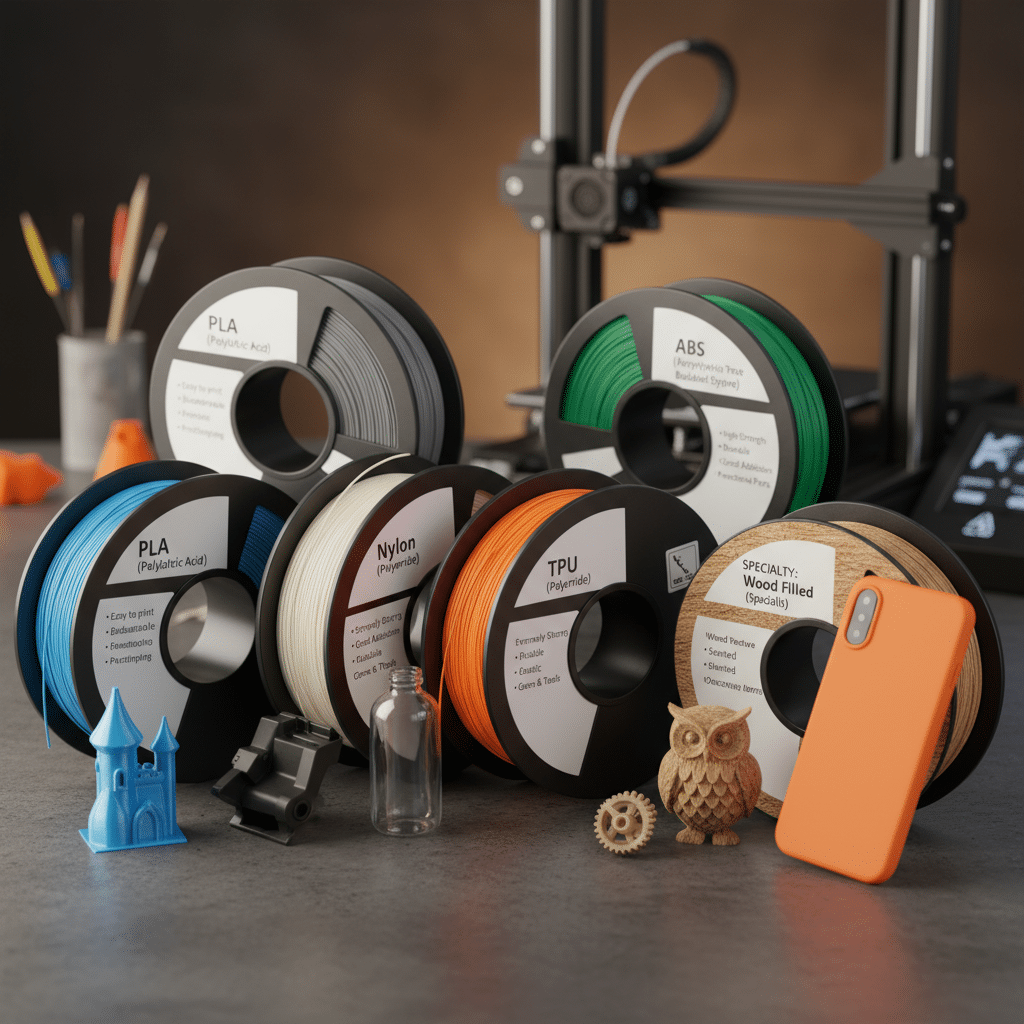
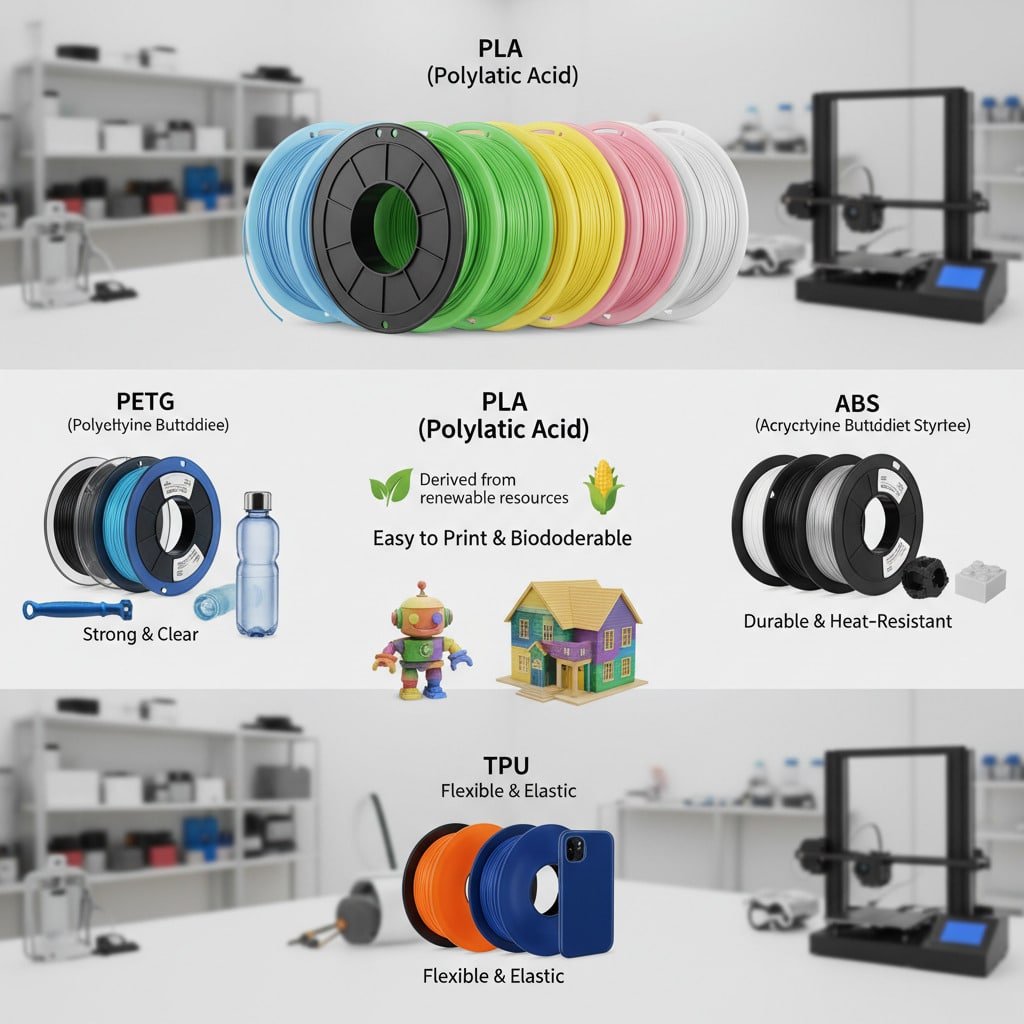
PLA is the easiest starting point for clean visual prints. PETG adds toughness and moisture resistance. ABS and ASA suit functional parts when an enclosure is available, with ASA usually preferred outdoors. TPU bends and absorbs impact. Nylon handles wear and repeated movement but must be kept dry. Polycarbonate is for high-heat, high-strength work on a capable machine.
| Material | Best use | Main advantage | Main limitation | Typical setup |
|---|---|---|---|---|
| PLA | Models, prototypes, decor | Easy detail and low warping | Low heat resistance | Works on most open printers |
| PETG | Brackets, organizers, containers | Tough and moisture resistant | Stringing and strong bed adhesion | Heated bed; dry spool helps |
| ABS | Indoor housings and fixtures | Impact and heat resistance | Warping and emissions | Enclosure and ventilation |
| ASA | Outdoor housings and mounts | Weather and UV resistance | Warping; higher setup demand | Enclosure and ventilation |
| TPU | Cases, feet, seals, dampers | Flexible and abrasion resistant | Slow, sensitive extrusion | Controlled filament path |
| PA / nylon | Gears, hinges, wear parts | Tough with low friction | Absorbs moisture quickly | Drying, dry box, often enclosure |
| PC | High-heat functional parts | Strength and temperature resistance | Difficult adhesion and warping | High-temperature enclosed printer |
These are material families, not identical formulas. A manufacturer’s PLA+ or high-flow PETG may behave differently from another brand’s standard version. Use the spool label and a tested printer profile as the final authority for temperature and cooling.
PLA: the sensible first material
PLA is reliable for scale models, figurines, presentation prototypes, organizers, and parts used at normal indoor temperatures. It holds small detail well and usually prints without an enclosure. That makes it useful when the priority is surface clarity rather than impact or heat performance.
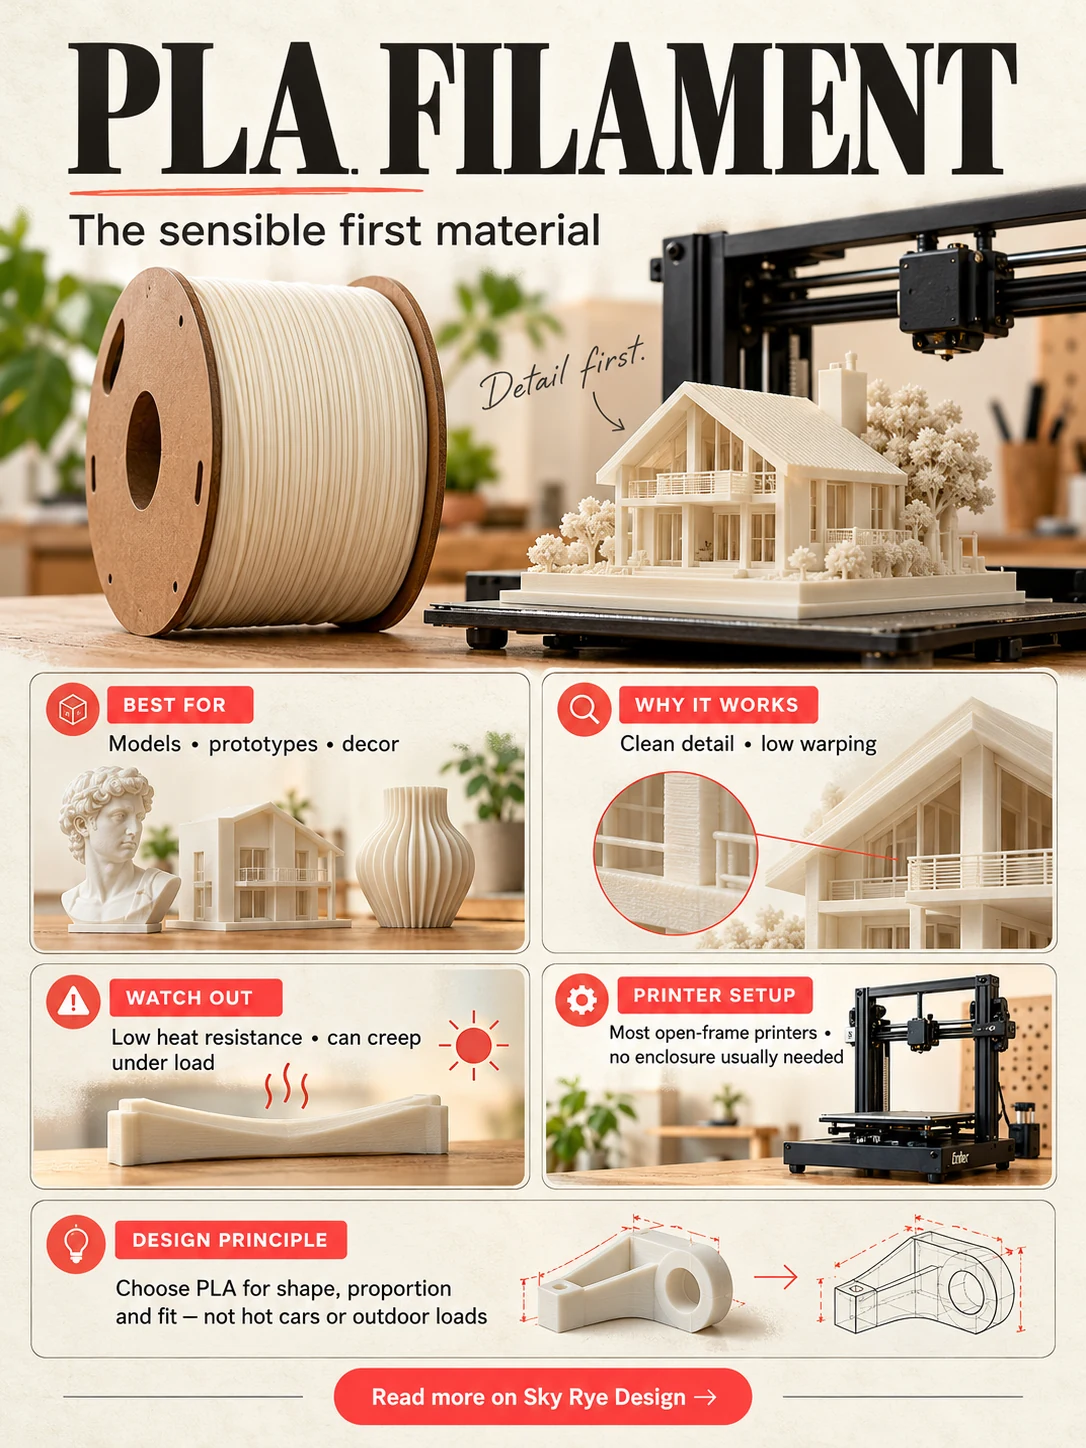
The limitation matters: standard PLA can soften in a hot car or near a sunny window, and a thin loaded part may creep over time. I use PLA when the print needs to communicate shape, proportion, or fit. I do not use it merely because it is already loaded when the part will carry weight or sit outdoors.
PETG: a tougher general-purpose option
PETG is a practical step up for tool holders, clips, housings, workshop organizers, and other parts that need more give than PLA. It resists water well and is less likely to shatter under a knock. It is still not a universal outdoor or high-temperature material; exposure, load, color, and the exact formulation all affect service life.
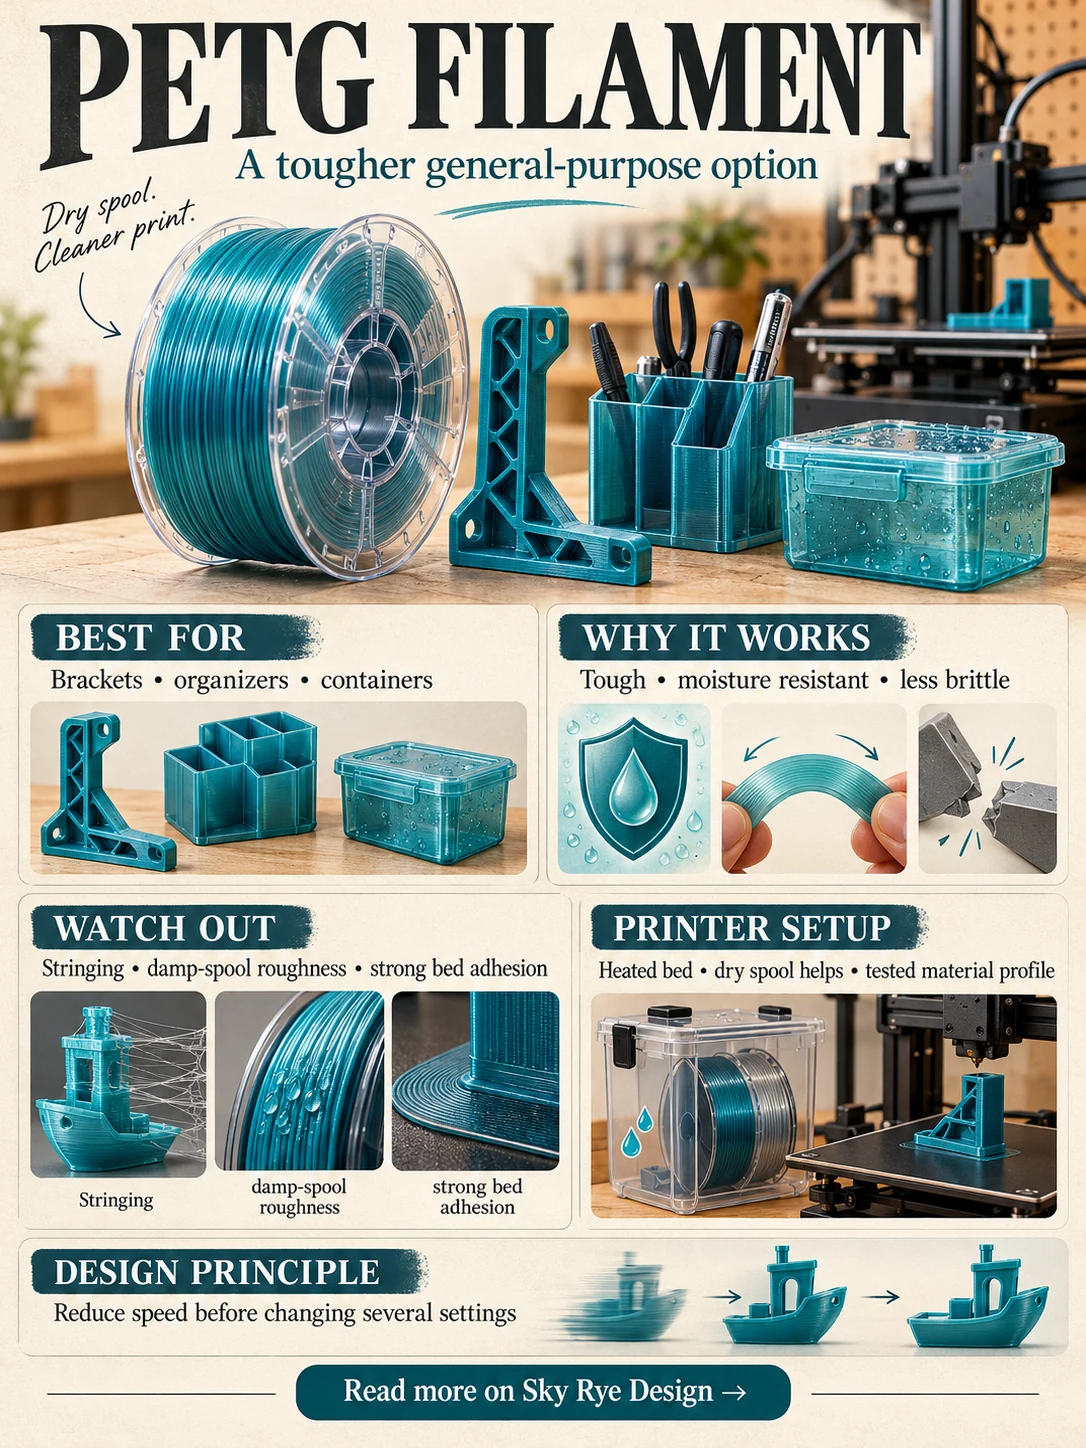
Most PETG problems are process problems. A damp spool produces rough surfaces and popping. Excess nozzle heat increases stringing. Too much first-layer squeeze can bond the print aggressively to smooth PEI. Start with the manufacturer’s profile, reduce speed before making several changes at once, and use the build-surface treatment recommended for your plate.
ABS and ASA: enclosed printing for functional parts
ABS remains useful for impact-resistant housings, fixtures, and parts that will be sanded, bonded, painted, or acetone-smoothed. ASA offers a similar printing class with better resistance to UV and weather, so it is usually the stronger candidate for exterior brackets, sensor covers, and garden hardware.
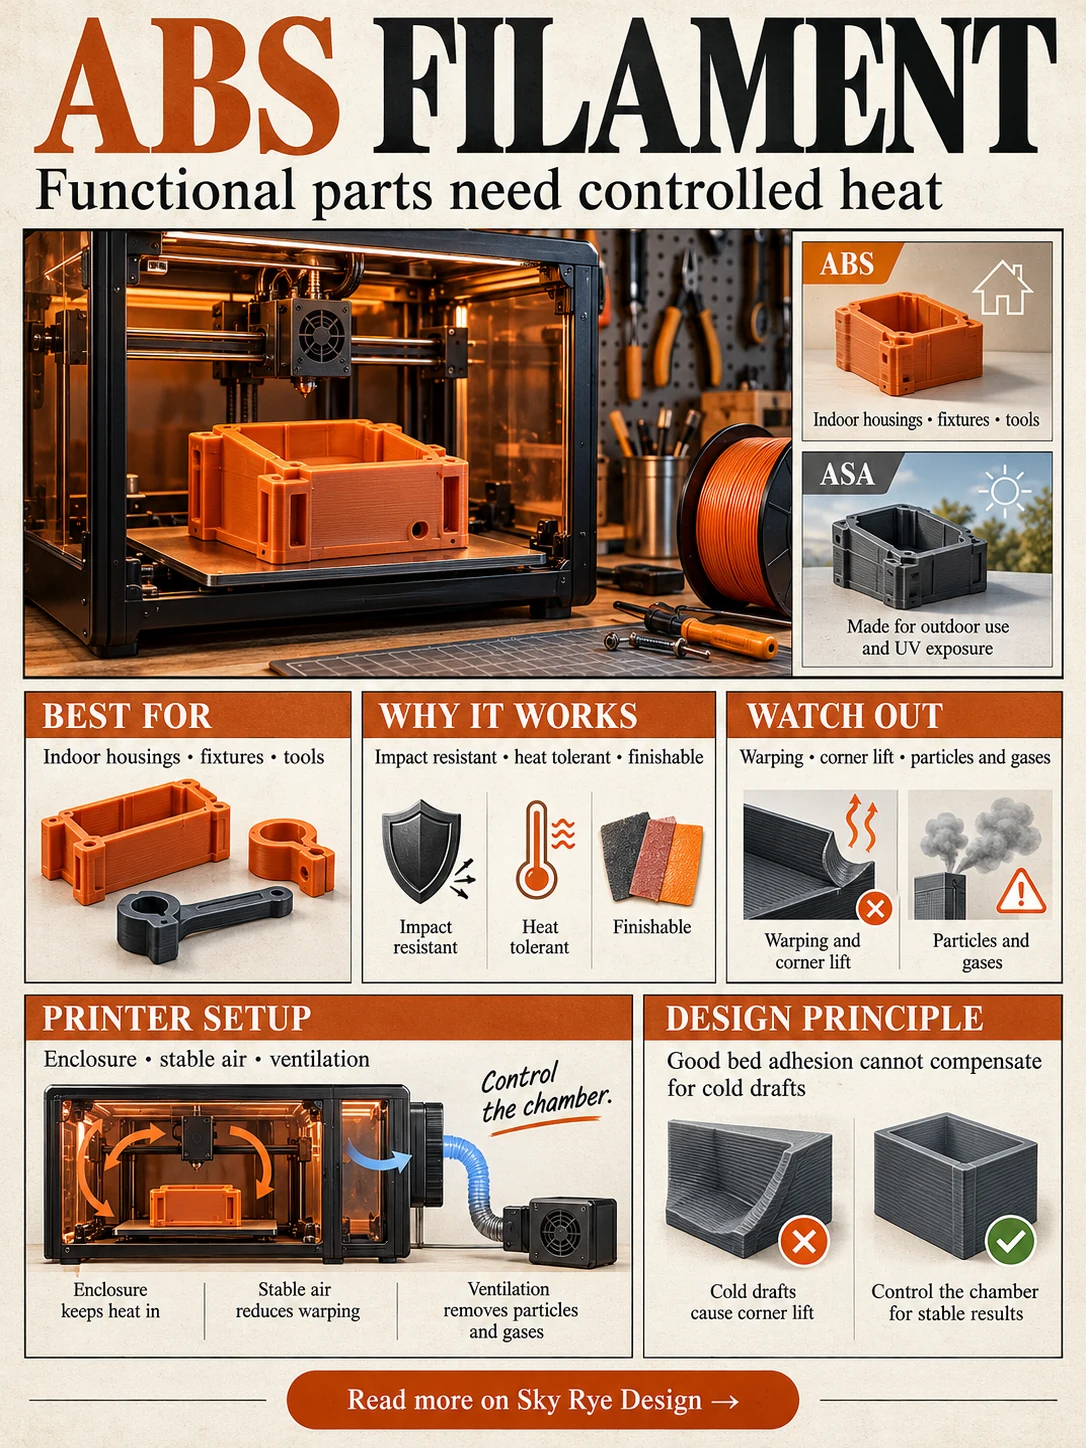
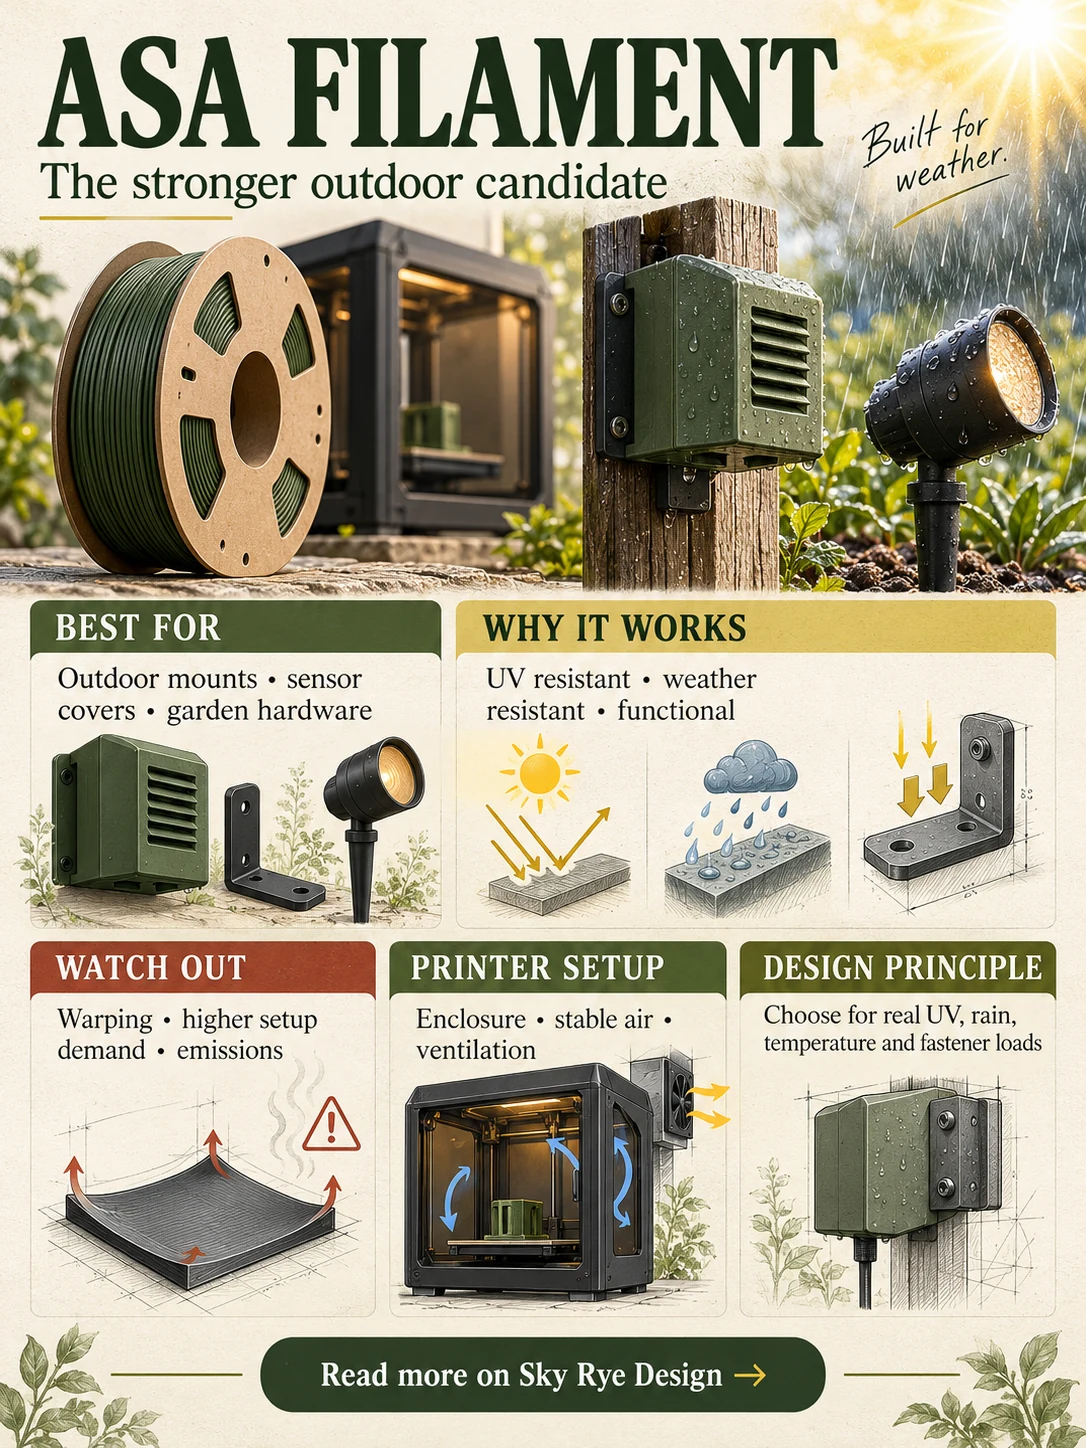
Both materials shrink as they cool. An enclosure is not a luxury for a large part; it keeps the air around the print stable and reduces corner lift and layer splitting. Good bed adhesion cannot compensate for cold drafts. Ventilation also belongs in the setup because heated filament can release particles and gases even when the odor seems mild.
TPU: flexible parts need a controlled filament path
TPU works for protective feet, cable strain relief, seals, phone cases, vibration dampers, and parts that must bend repeatedly. Shore hardness matters: a firmer TPU is easier to feed than a very soft grade. The model also needs room to flex; copying the wall thickness from a rigid PLA part can produce an unexpectedly stiff result.
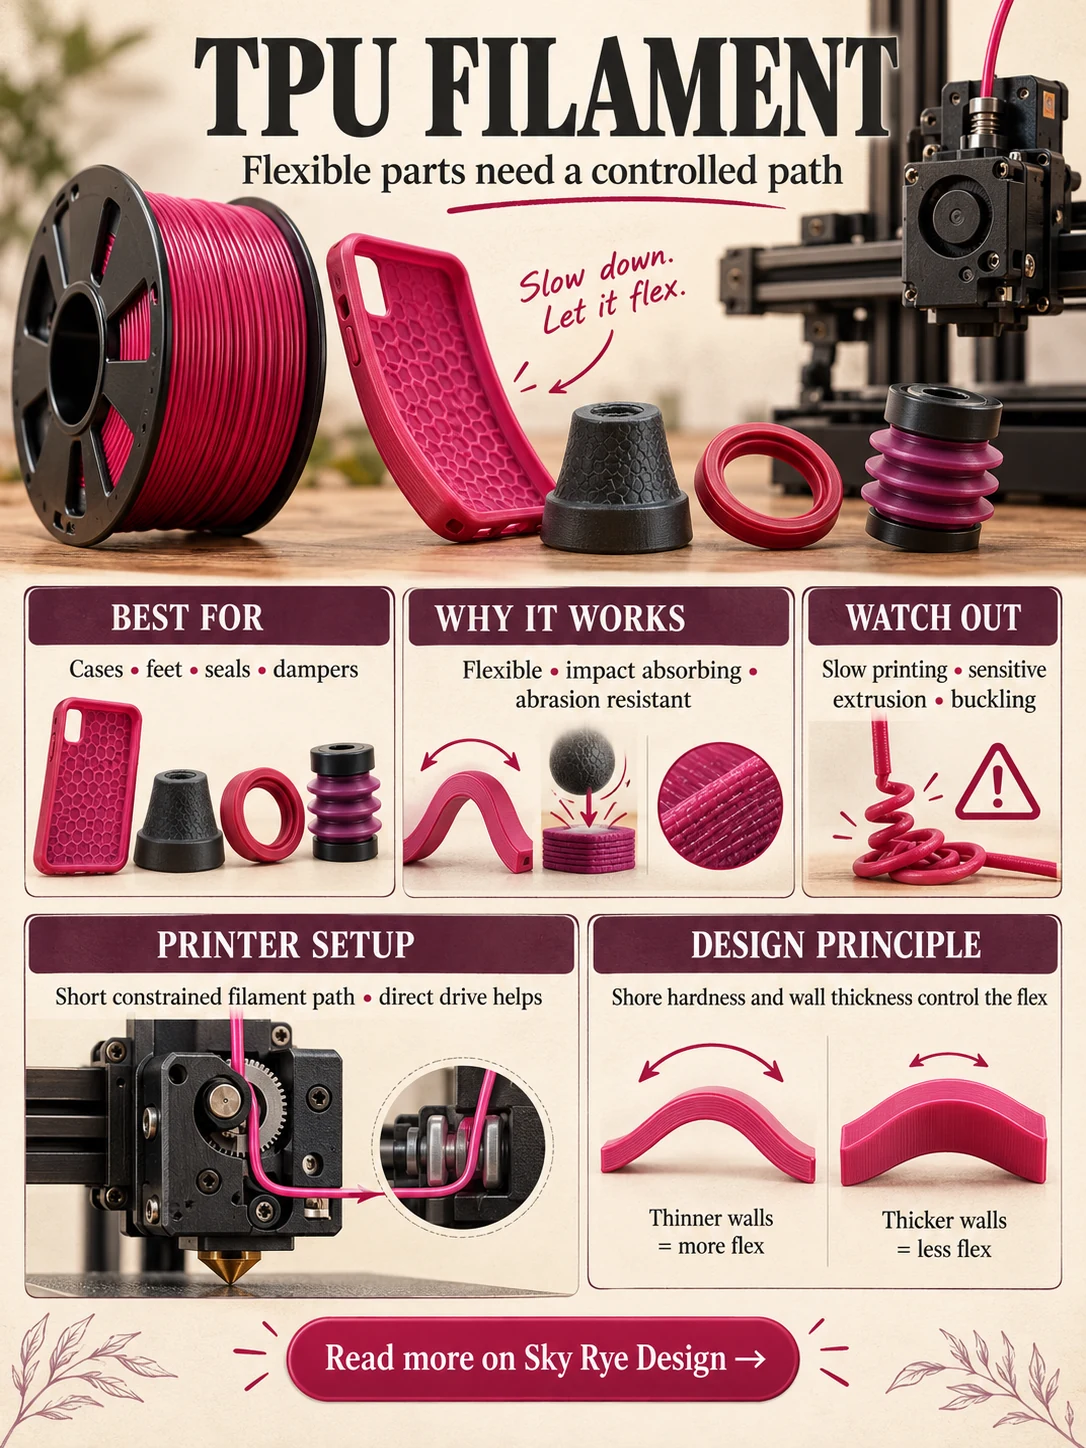
Print slowly and remove unnecessary resistance between the drive gears and nozzle. A direct-drive extruder helps, but a well-constrained Bowden path can handle some firmer flexible filaments. If the extruder clicks or the strand buckles, lower speed and volumetric flow before adding more tension.
Nylon and polycarbonate: demanding materials for demanding parts
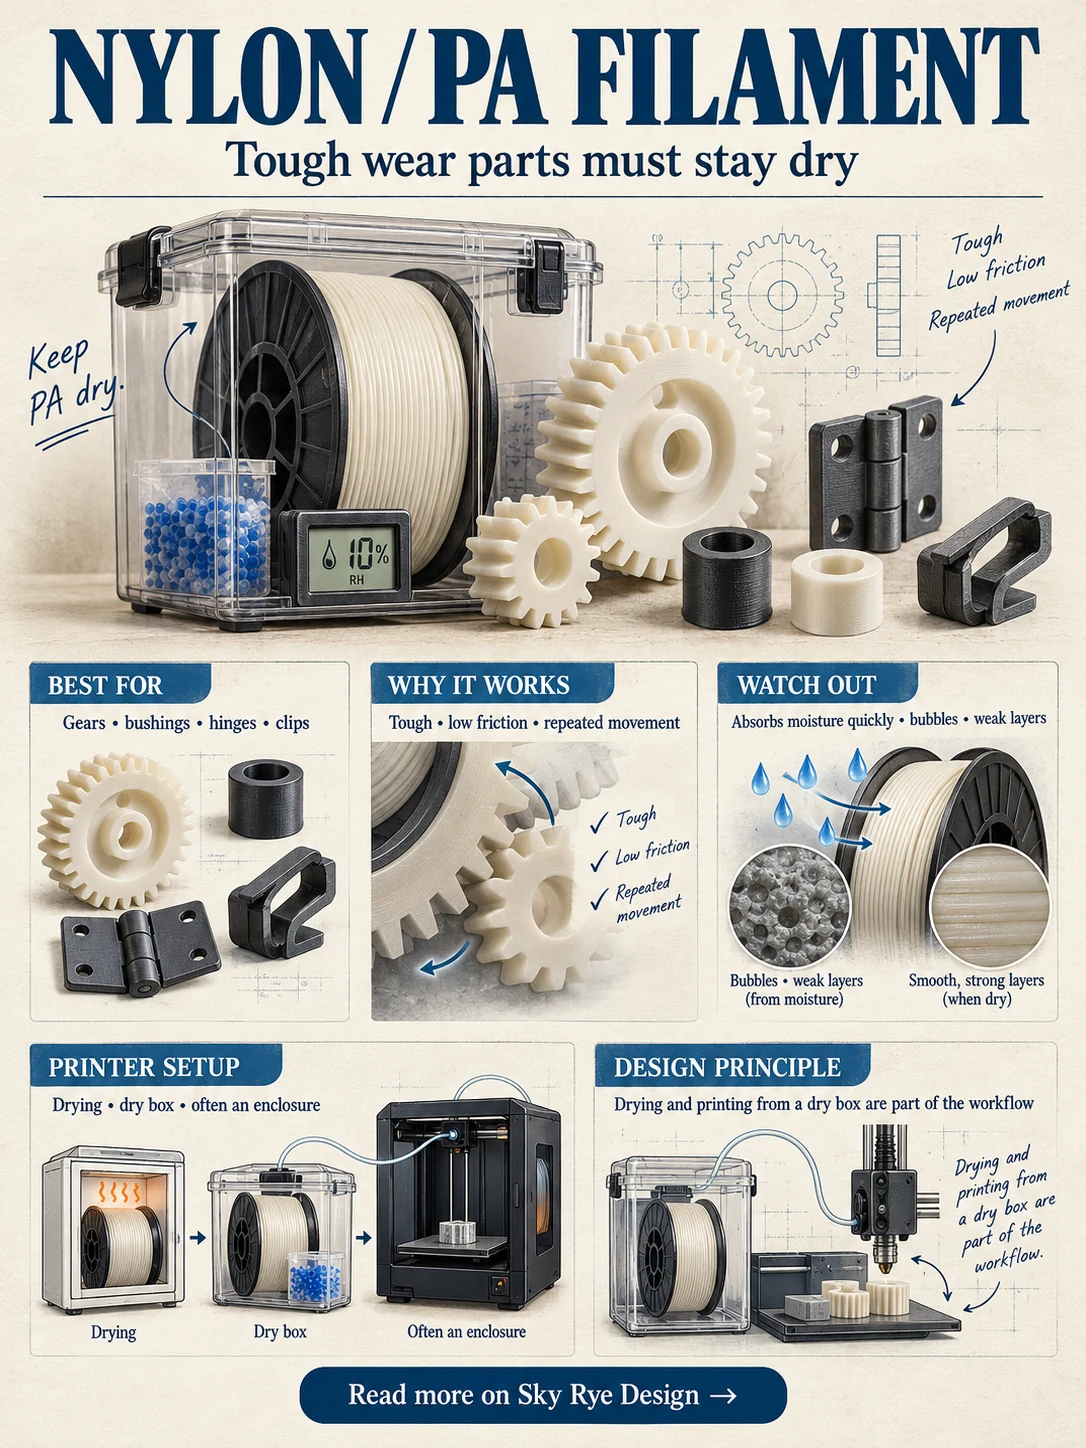
Nylon, often marked PA, is valuable for gears, bushings, hinges, clips, and wear parts because it combines toughness with a relatively low-friction surface. Its weakness is moisture. Nylon can absorb enough water from room air to print with bubbles, weak layers, and a rough finish, so drying and printing from a dry box are part of the workflow.
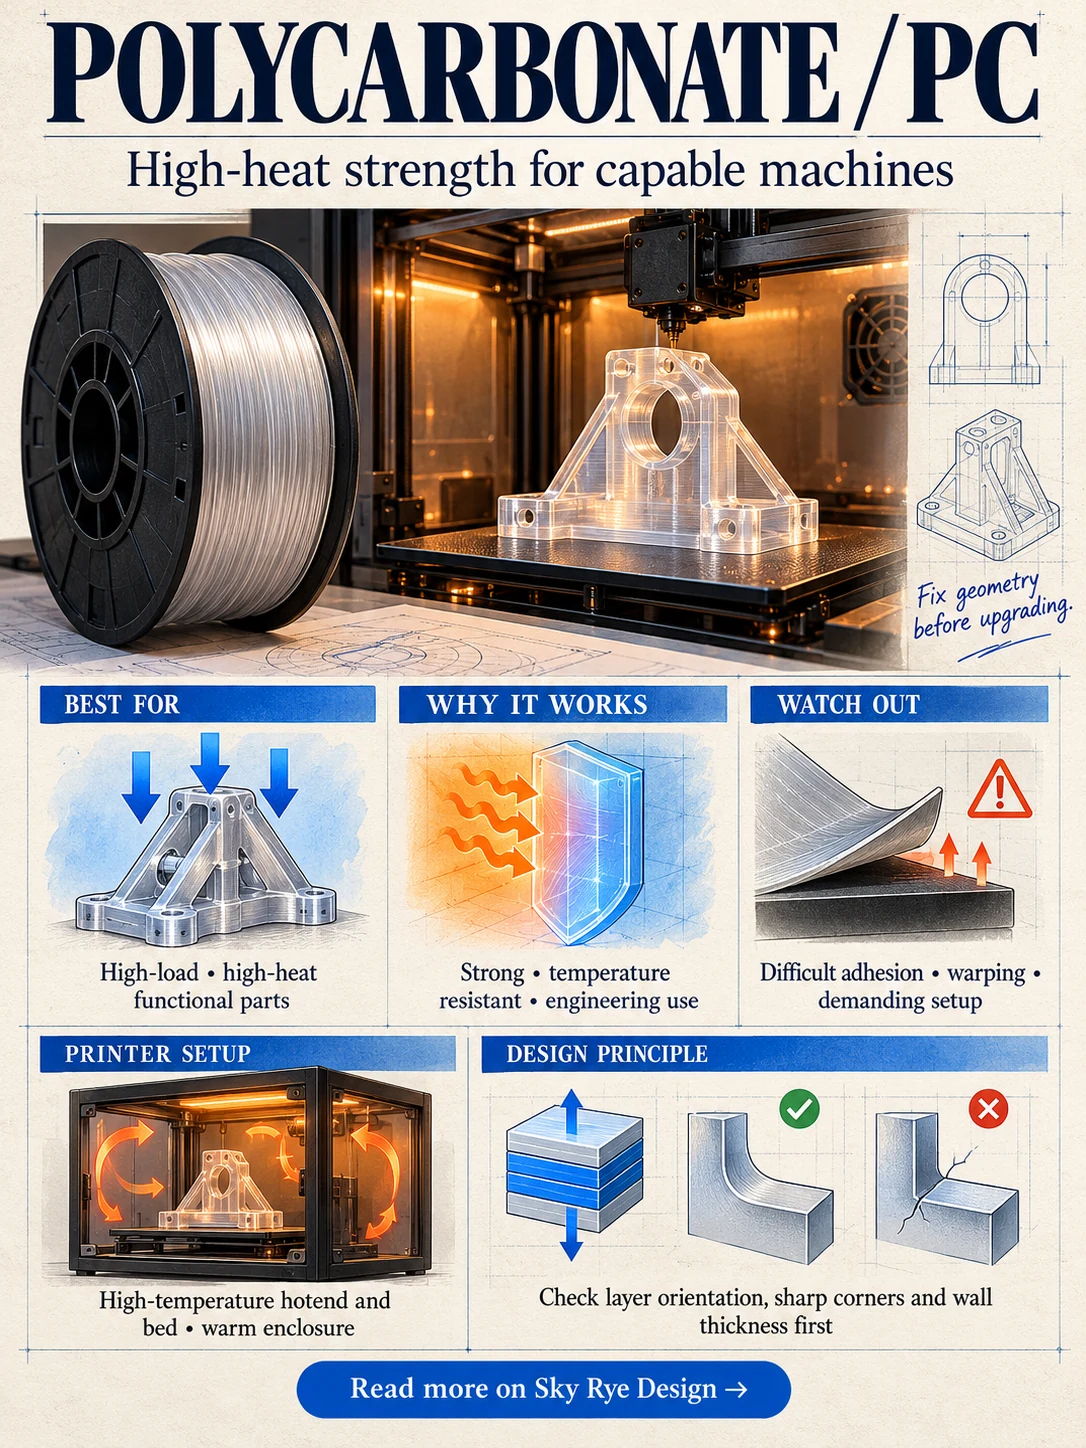
Polycarbonate can handle higher loads and temperatures, but it asks more from the printer: high nozzle and bed capability, strong adhesion, controlled cooling, and a warm enclosure. It is not a sensible upgrade simply because a part failed in PLA. First check whether the failure came from layer orientation, a sharp internal corner, or insufficient wall thickness.
Composite and specialty filaments
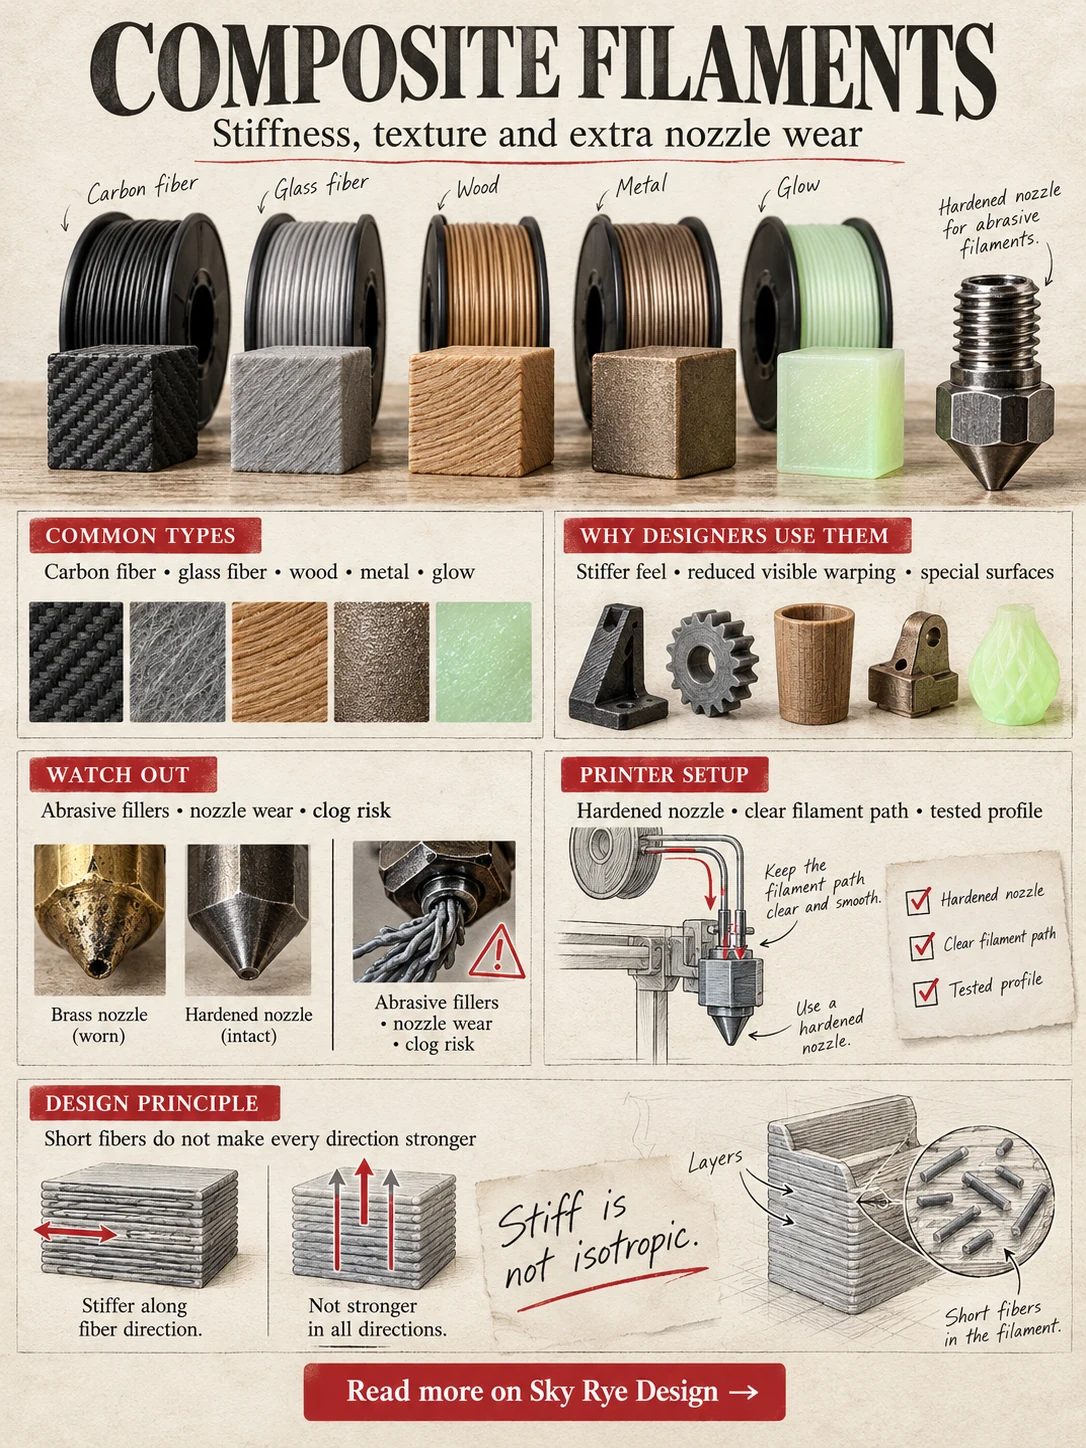
Carbon-fiber and glass-fiber blends can improve stiffness and reduce visible warping, but the short fibers do not make every part stronger in every direction. They are abrasive and usually require a hardened nozzle. Wood-, metal-, and glow-filled filaments can also wear a standard brass nozzle and may clog a small or partially obstructed opening.
Support materials such as PVA or BVOH solve a different problem: they create removable support for complex geometry. They are moisture sensitive, add cost, and require compatible multi-material hardware. Buy a specialty spool because the project needs its specific behavior, not because the label sounds advanced.
Choose filament by the project, not the spool color
| Project requirement | Start with | Check before printing |
|---|---|---|
| Clean visual prototype | PLA | Heat exposure and long-term load |
| Tough indoor bracket | PETG or ABS | Stiffness, creep, enclosure availability |
| Outdoor mount | ASA | UV, rain, temperature, fastener load |
| Flexible case or foot | TPU | Shore hardness and wall thickness |
| Gear or living hinge | PA / nylon | Drying, friction, fatigue direction |
| High-temperature fixture | PC or engineering blend | Actual service temperature and printer limits |
| Stiff composite prototype | Fiber-filled PLA, PETG, or PA | Hardened nozzle and anisotropic strength |
Material cannot rescue weak geometry. Thin walls, sharp corners, poor layer orientation, and an unsupported snap-fit can fail in an expensive polymer just as easily as in PLA. Use the dimensional rules in our guide to designing parts for 3D printing, then confirm wall thickness and clearances with these 3D printing design rules.
Check printer compatibility before ordering a spool
- Nozzle temperature: the hotend must reach and safely hold the material’s specified range.
- Bed temperature: ABS, ASA, PC, and many nylon blends need more bed heat than entry-level machines provide.
- Enclosure: it stabilizes the print environment for shrink-prone materials; never enclose electronics that are not designed for the heat.
- Nozzle material: carbon fiber, glass fiber, glow pigment, and some fillers can wear brass quickly.
- Extruder path: flexible filament prints more predictably when the path from drive gear to hotend is short and constrained.
- Spool system: some automatic material systems cannot feed soft TPU or rough, brittle, or oversized spools reliably.
Hardware changes should solve a measured limitation. If abrasive materials, higher flow, or a more controlled feed path are genuinely needed, compare the options in these practical 3D printer upgrades instead of replacing several parts at once.
Drying and storage are part of material selection
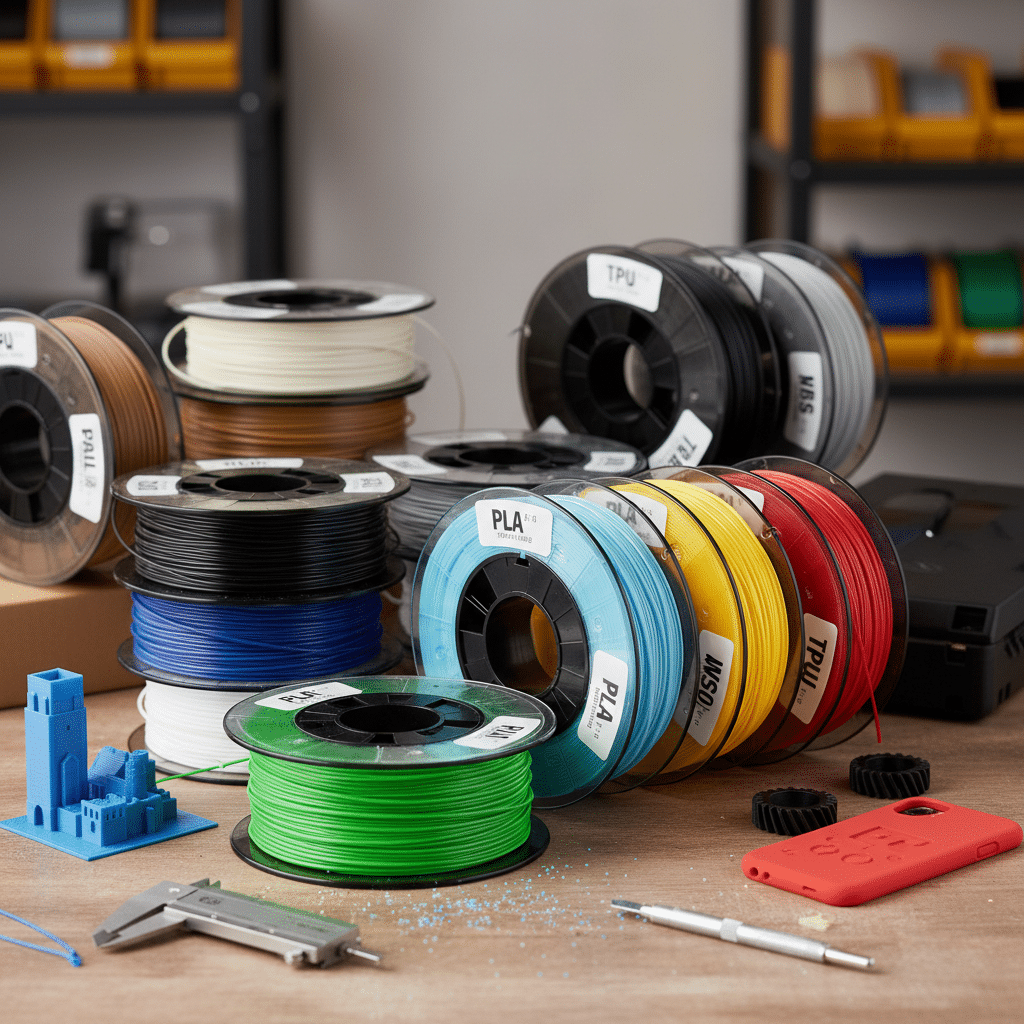
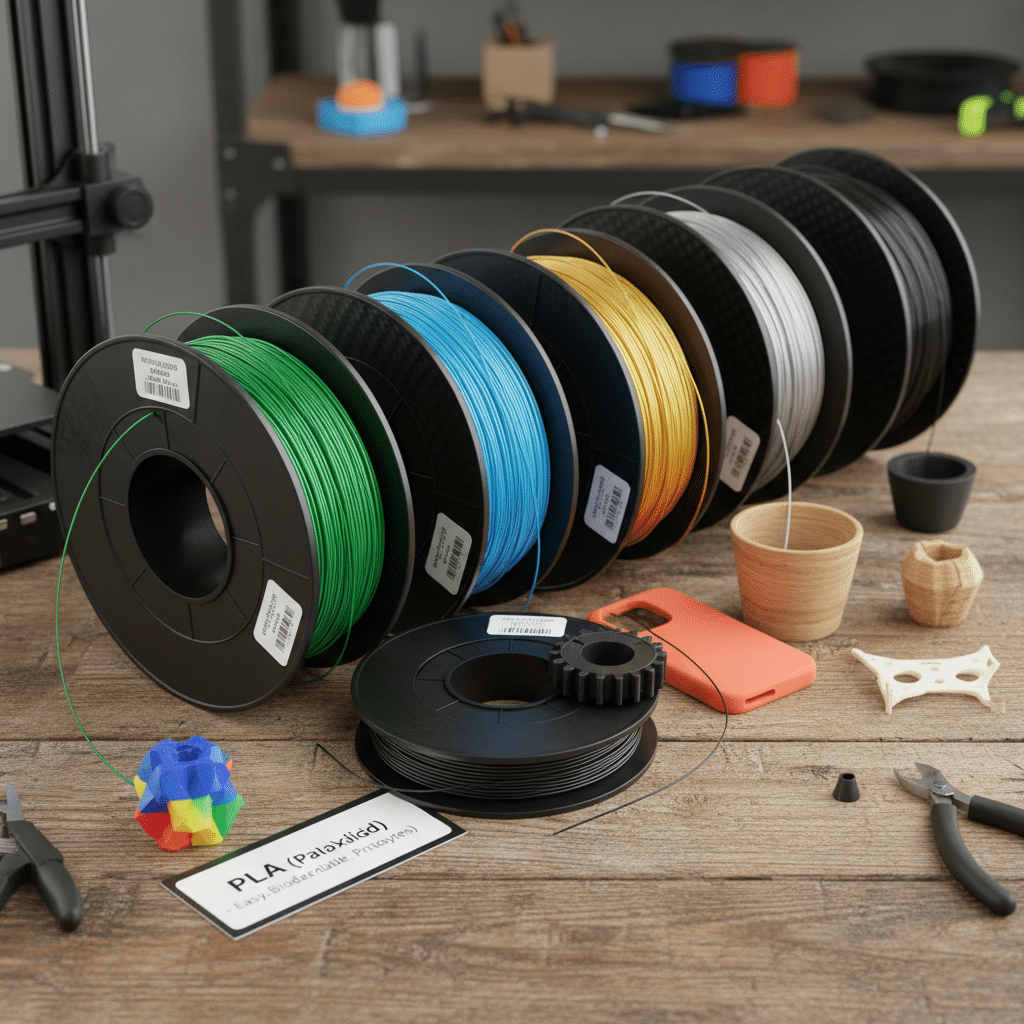
A sealed bag does not guarantee a dry spool after weeks on a shelf. PETG, TPU, nylon, PC, PVA, and many composites can absorb moisture; nylon and soluble supports are especially sensitive. Common signs are popping at the nozzle, steam, rough walls, excessive stringing, and weak or inconsistent extrusion.
Store open spools in a sealed container with fresh desiccant and a humidity indicator. Dry only at the temperature and time recommended for that exact product. A kitchen oven can overshoot badly and may contaminate a food appliance, so use equipment intended for filament or a controlled dehydrator setup.
Treat temperature ranges as starting points
Filament guides show why one universal temperature chart is misleading. The official Prusa filament material guide lists broad hardware and temperature ranges across PLA, PETG, ASA, ABS, flexible materials, nylon, PC, and composites. Brand chemistry, nozzle type, speed, layer height, and part cooling still change the best setting.
- Load the manufacturer’s profile for the exact material family.
- Print a small temperature or flow test using the intended layer height.
- Change one variable at a time and record the result.
- Validate with a functional coupon that copies the real wall, bridge, hole, or snap-fit.
- Save the successful profile with the brand, color, nozzle, and date.
Ventilation belongs in the print plan
Desktop printers can release ultrafine particles and volatile compounds, and the amount depends on the printer, polymer, color, additives, and temperature. The US National Institute for Occupational Safety and Health recommends a hierarchy of controls, including material substitution, isolation, ventilated enclosures, local exhaust, and limiting time near active printers; see its safe 3D printing guidance.
Do not treat a lack of odor as proof that a print is emission-free. Follow the filament safety data sheet and printer instructions, keep food away from the work area, and use appropriate protection for sanding, solvents, carbon- or glass-filled materials, and other post-processing. Our 3D print post-processing guide covers the finishing sequence once the part is off the bed.
Common filament-selection mistakes
| Mistake | Why it fails | Better decision |
|---|---|---|
| Choosing by strength claims alone | Layer direction and geometry control failure | Test the real load and orientation |
| Using PLA for a hot car | The part can soften and creep | Measure service temperature and compare ASA, ABS, PC, or another qualified material |
| Printing wet filament hotter | Heat does not remove moisture during extrusion | Dry the spool correctly, then retune |
| Buying fiber-filled filament for strength | It may add stiffness while remaining weak across layers | Check the technical data and print orientation |
| Ignoring the enclosure requirement | Drafts cause warping and layer splitting | Choose a compatible material or control the chamber |
| Copying settings from another brand | Additives and flow behavior vary | Start with the product profile and test one variable at a time |
Put the material choice into a real project
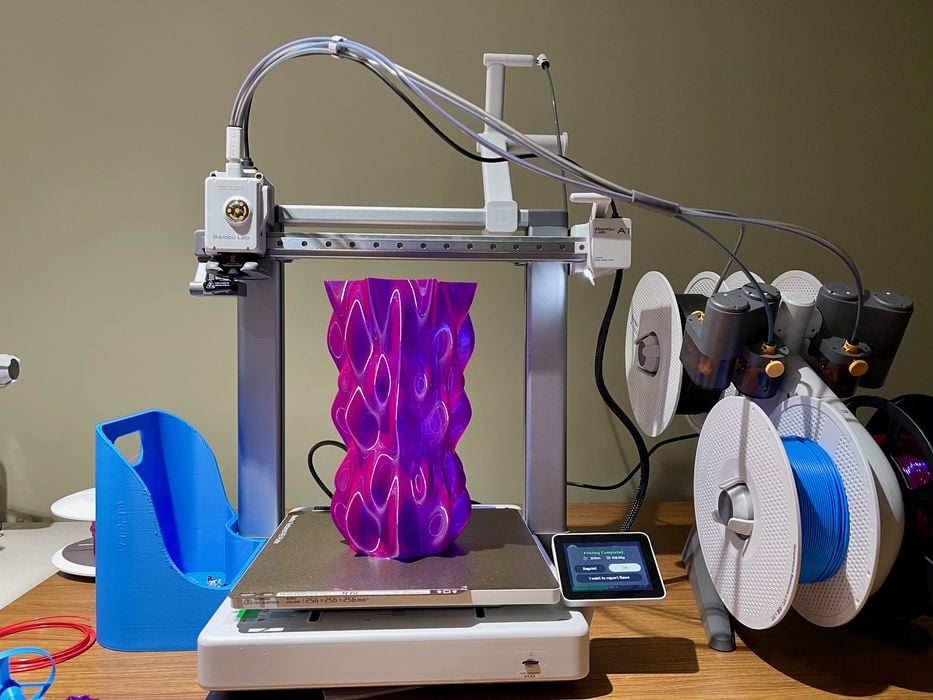
For a first test, pick a small object that reveals fit, overhangs, and surface quality without using half a spool. These easy 3D prints and small fast prints are useful calibration projects rather than decorative torture tests.
Once the profile is stable, move to a part with a clear job. Browse useful 3D printed items for functional ideas, or use the larger 3D printing ideas collection to compare decor, prototypes, tools, and creative projects.
If the model comes from someone else, read the license and the designer’s material notes before slicing. Our introduction to STL files for 3D printing explains what the file contains and what still has to be decided in the slicer.
3D printer filament types FAQ
What are the main 3D printer filament types and their uses?
PLA suits detailed models and easy prototypes; PETG works well for tougher indoor parts; ASA is a stronger outdoor choice; ABS handles impact and heat in an enclosure; TPU is flexible; nylon suits wear parts; and PC is reserved for demanding high-temperature prints.
Why is PLA usually the best filament for beginners?
PLA usually needs less bed heat, warps less than engineering plastics, and works with most open-frame printers. It is a sensible first material for visual prototypes, organizers, models, and decorative parts, but it is a poor choice for a hot car, direct sun, or a load-bearing part.
How does PETG compare with PLA and ABS?
PETG is tougher and more heat tolerant than standard PLA, while usually being easier to print than ABS. It can string, absorb moisture, and bond aggressively to some build surfaces. Use a tested printer profile and a suitable release layer instead of copying another material’s settings.
Should I use ABS or ASA for functional parts?
Both can produce tough functional parts and normally benefit from an enclosure. ASA is generally the better choice for outdoor exposure because it has stronger UV and weather resistance. ABS remains useful for indoor housings, fixtures, and parts that will be sanded, bonded, or vapor-smoothed.
Which filament should I choose for outdoor or high-heat parts?
For outdoor parts, start with ASA when the printer can handle an enclosure and the required bed temperature. PETG can work for less demanding outdoor jobs, but brand formulations vary. For higher heat, compare ASA, ABS, PC, or engineering nylon against the actual service temperature and load.
Choose the least demanding material that meets the real load, temperature, flexibility, and exposure requirements. That usually produces a more reliable part, a shorter calibration cycle, and a print profile you can reproduce later.
- 43shares
- Facebook0
- Pinterest43
- Twitter0
- Reddit0